Processing Thin CRGO (0.18 to 0.23 mm): What Changes on a Cut-to-Length Line
Thinner grain-oriented steel lowers core loss but is harder to feed, cut and stack. This article covers what actually changes on the line when you move from 0.27 or 0.30 mm to 0.18 or 0.20 mm, and what to specify so the line copes.
Transformer loss standards keep tightening, and the steel makers’ answer has been thinner grain-oriented grades: 0.23 mm, 0.20 mm, 0.18 mm, with 0.15 mm available for the lowest-loss designs. Thinner sheet cuts eddy-current loss, which scales with the square of thickness, so a core built from 0.20 mm material has a clear advantage over the same core in 0.27 mm. The cost is that thin material is harder to handle at every step of the core shop, and the cut-to-length line is where the difference shows first.
Four things that change
1. The strip is easier to deflect
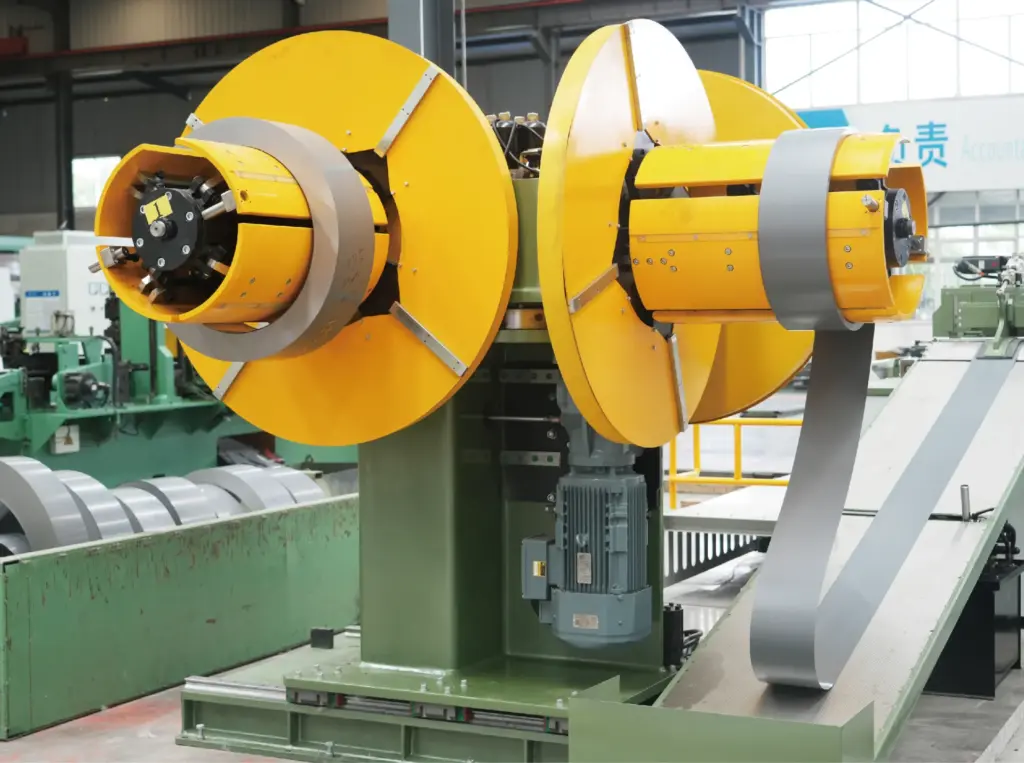
Feed rollers push the strip forward; a thin strip resists that push less and is more likely to bow, wander or buckle between the feed and the shear, especially when the line stops and starts. The remedies are a servo feed with controlled acceleration, edge guides set close to the strip, short unsupported spans between stations and a decoiler that keeps back-tension steady. On SREE lines the feed axis is servo-driven as standard, and for material at the thin end of the range, 0.15 mm in particular, we specify the feed and guiding for it at the enquiry stage; the line selector flags this automatically when 0.15 mm is entered.
2. Burr becomes a larger fraction of the sheet
A burr of 0.02 mm is 7 percent of a 0.30 mm sheet and 11 percent of a 0.18 mm sheet. The same absolute burr therefore does more damage to the stacking factor and the interlaminar insulation on thin material. Holding burr down on thin sheet needs a sharper blade, a clearance set specifically for the gauge, and a rigid shear frame, because thin sheet is dragged into the clearance more easily than thick sheet. The line specification of ≤0.02 mm applies across the thickness range, but on thin material it has to be maintained more attentively: blade regrinding intervals shorten and clearance must be reset when the gauge changes.
3. There are more pieces per core
For the same core cross-section, moving from 0.30 mm to 0.20 mm means 50 percent more laminations. The line cuts the same tonnage but half as many more pieces, and every piece is a cut cycle. On a step-feed line, output per shift in tonnes falls; on a continuous-feed line it falls less, because output there is limited by strip speed rather than by cycle count. This is one of the reasons plants that move to thin grades tend to move to high-speed lines at the same time; see standard vs high-speed lines. It also means the sorting end of the line and the stacking operation have more to handle, which is where automatic stacking starts to pay for itself.
4. Handling after the cut
Thin laminations are more easily bent when they drop onto the stacking table, more easily damaged by forklift handling, and slower to stack by hand because each piece is lighter and less stiff. Softer drop heights on the stacking tables, and either a stacking line or a cut-and-stack combined line that never lets the piece leave the machine, are the usual answers.
What to specify
| Item | Why it matters on thin material | What to ask for |
|---|---|---|
| Thickness range | Feed, punch and shear settings are designed for a range, not a point | State the full range you will run, including the thinnest grade you expect in three years |
| Feed and guiding | Thin strip deflects and wanders more | Servo feed with controlled acceleration; close edge guiding; short spans |
| Shear | Burr is a larger fraction of sheet thickness | Rigid frame, blade clearance set per gauge, defined regrind procedure |
| Output basis | More pieces per tonne | Ask for output in laminations per hour at your piece lengths, not only in m/min |
| Stacking end | More pieces to handle, each more fragile | Consider automatic stacking or a combined line at the same time |
The SREE range
Our cut-to-length lines cover 0.18 to 0.35 mm as standard, which spans the common CRGO grades from conventional 0.35 and 0.30 mm through 0.27 and 0.23 mm to the 0.20 and 0.18 mm high-permeability grades. 0.15 mm is available on request with the feed and guiding specified for it. The cutting tolerances are the same across the range: length ±0.2 mm per 2 m, mitre angle ±0.02°, burr ≤0.02 mm.
Frequently asked questions
Can an existing line be adjusted for thinner steel?
Often, within the line’s design range: blade clearance, feed parameters and guiding are adjustable. Going below the design range, for example to 0.15 mm on a line specified for 0.23 to 0.35 mm, should be discussed with the builder first, because feed and guiding may need changes.
Does thin steel cut faster or slower?
Strip speed is the same; what changes is the number of pieces per tonne, so tonnes per hour fall while pieces per hour stay roughly constant on a given line.
Is the burr specification different for thin material?
The specification is the same, ≤0.02 mm, but it needs more maintenance attention to hold on thin material.
Sizing a line for your core shop?
Send strip widths, thickness and monthly tonnage. You get a line proposal with knife layout and floor plan, or use the online selector to narrow the series first.