Cutting Tolerances That Matter for Transformer Cores: Angle, Length and Burr
Three numbers on a cut-to-length line datasheet decide how good the finished core will be. Here is what each one does to no-load loss, noise and stacking, what the figures should look like, and what to ask a supplier before you believe them.
A cut-to-length line datasheet carries three tolerances: the angle of the mitred cut, the length of the lamination, and the height of the burr left by the shear. They look like small numbers, and they are, but each one turns directly into a property of the finished transformer. Angle error shows up as no-load loss and noise. Length error shows up as an uneven stack and a core that does not match its drawing. Burr shows up as interlaminar shorts and a lower stacking factor. This article explains each one and what to look for when comparing lines.
Angle: why 0.02° is worth arguing about
Stacked cores are built with 45° mitred joints so that the flux crosses from limb to yoke along the rolling direction of the steel, where grain-oriented material has its lowest loss. At the joint the flux has to jump the gap between the two pieces. Any deviation of the cut from 45° opens that gap on one side of the joint: over the width of a lamination, an angle error of a few hundredths of a degree already produces a gap of tenths of a millimetre at the edge.
The gap matters twice. First, the flux crowding around it raises the local loss and the magnetising current, which appears in the test report as higher no-load loss. Second, the same gap is a source of magnetostriction noise, which is why a core cut on a worn or misaligned shear is often audibly louder than one cut on a good line, with the same steel and the same design.
SREE lines hold the mitre angle to ±0.02°. The number depends on three things: the accuracy of the shear rotation, the rigidity of the shear frame so that the blade does not deflect under load, and the edge guiding that keeps the strip square to the shear. A line that meets the figure when new should meet it years later if the blade clearance is maintained; this is a maintenance item, and we cover it in the operator training.
Length: tolerance per reference length
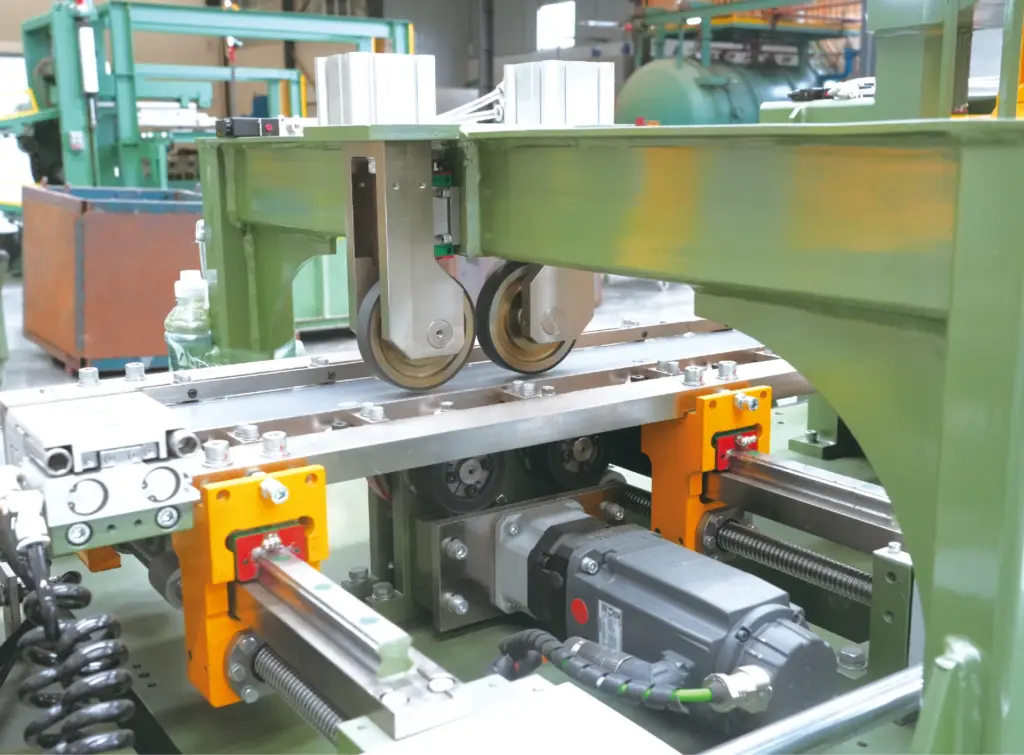
Length tolerance is quoted per reference length, because the error grows with the length of the piece: ±0.2 mm per 2 m on most of our lines, ±0.2 mm per 3 m on the 1000 class. The figure is set by the feed axis, which is a servo axis with a measuring roller, and by how well the strip is held against slipping during acceleration.
What a length error does in the core: the outer limbs and the yokes must match each other in length to close the window; the step-lap layers must differ from each other by exactly the design step. If lengths drift within a batch, the stack either does not close cleanly at the corners or the steps no longer line up, and the assembler compensates by hand, which costs time and rarely gives the designed joint.
When comparing datasheets, check that the reference length is stated. A tolerance of ±0.2 mm without a reference length is not a specification.
Burr: the edge you cannot see
Shearing leaves a small raised edge on the underside of the cut. On a 0.27 mm lamination a burr of 0.05 mm is nearly a fifth of the sheet thickness, so it is not negligible. Two things happen in the stacked core. The burr punctures the insulating coating of the neighbouring lamination and creates an electrical path between sheets; enough of these paths, and eddy currents circulate through several laminations at once, raising loss. And the burr holds the sheets apart, so the same number of laminations makes a taller stack, which is measured as a lower stacking factor and means a heavier core for the same flux.
Our lines are specified for a burr height of 0.02 mm or less. Burr is a function of blade sharpness, blade clearance set for the sheet thickness, and the shear geometry. It is the tolerance most likely to deteriorate in service, which is why blade regrinding and clearance setting are part of scheduled maintenance rather than something to do when the core builders complain.
The three figures together
| Tolerance | SREE specification | What it affects in the transformer | What sets it on the line |
|---|---|---|---|
| Mitre angle | ±0.02° | Joint gap: no-load loss, magnetising current, noise | Shear rotation accuracy, frame rigidity, edge guiding |
| Length | ±0.2 mm per 2 m (per 3 m on the 1000 class) | Window closure, step-lap alignment, hand correction at assembly | Servo feed axis and measuring roller, strip grip |
| Burr height | ≤0.02 毫米 | Interlaminar insulation, eddy-current loss, stacking factor | Blade sharpness and clearance, shear geometry |
What to ask before you believe the numbers
Tolerances only mean something together with the way they were measured. Before comparing two offers on their figures, ask each supplier:
- On what material and thickness was the figure measured? Thin, high-grade steel behaves differently from 0.35 mm in the shear.
- Over what piece length, and how many pieces? A single good piece proves little; a sample of a full programme proves the line.
- How was the angle measured, and with what instrument? Ask for the test protocol, not just the result.
- Is the figure a guaranteed acceptance value or a typical value? The two are often quoted with the same number.
- Can the supplier cut a sample from your drawing, on your grade of steel, before acceptance?
A test cut from your own drawing, on your grade of steel, can be written into the pre-delivery acceptance of an SREE line; ask for it when you specify the line and the measured values go into the acceptance record. If a supplier will not do this at all, treat the datasheet figures as marketing.
Keeping the tolerances over the life of the line
All three figures depend on maintenance. The shear blade needs regrinding at intervals set by tonnage and material, and the clearance has to be reset after each regrind and whenever the sheet thickness changes. The measuring roller on the feed axis needs to be kept clean and checked against a reference length. Edge guides wear and need adjustment. None of this is difficult, but a line that is run without it will drift out of the datasheet within a year, and the core test bench will be the first to notice.
Specifications for each line, including these tolerances, are on the standard and high-speed cut-to-length line pages, and datasheets can be downloaded from the technical resources page.
Frequently asked questions
Which of the three tolerances is most important?
For no-load loss and noise, the angle. For assembly time, the length. For loss and core weight together, the burr. A good line holds all three; a worn line typically loses the burr figure first.
Does thinner steel need tighter tolerances?
The tolerances stay the same, but they are harder to hold: burr height becomes a larger fraction of sheet thickness and the strip is easier to deflect in the feed. See processing thin CRGO.
Can these tolerances be checked on site after installation?
Yes, and they should be, as part of the site acceptance test on your material with your drawings.