How to Choose a Cut-to-Length Line Width Class (200 to 1000) for Your Transformer Cores
The width class is the first and most consequential decision when buying a cut-to-length line. Four questions settle it: the widest lamination you build, the holes you punch, the tonnage you run, and the floor you have.
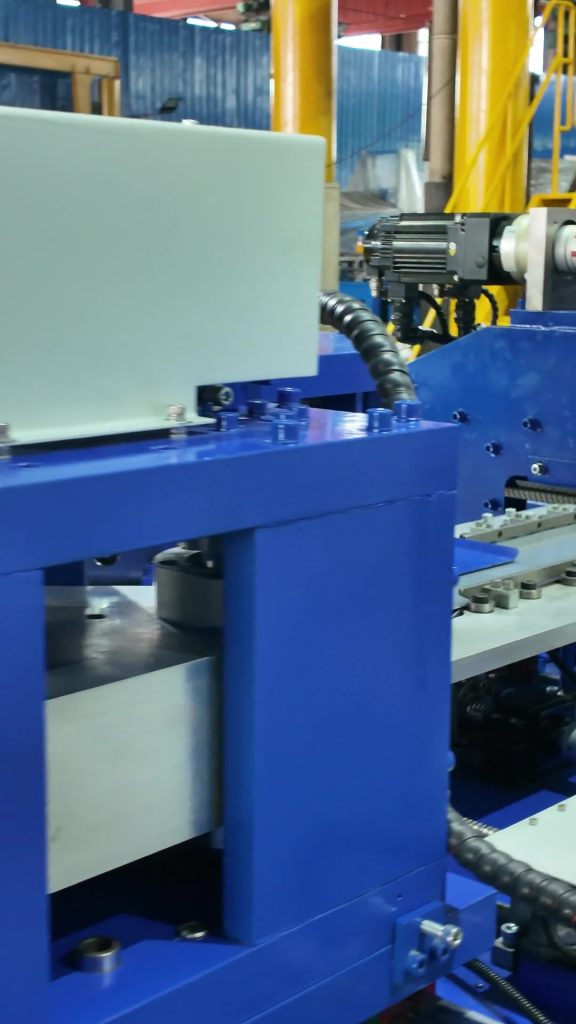
Cut-to-length lines are sold by width class: 200, 300, 400, 600, 800 and 1000 in the SREE range. The number is the nominal maximum strip width in millimetres, and it fixes most of the machine: the width of the feed rollers, the length of the shear blade, the size of the V-notch punch, the decoiler capacity and, with them, the footprint and the price. Getting it right is more important than any other single choice, because a line that is too small cannot cut your largest core, and a line that is too large costs money and floor space on every smaller core you ever cut.
We use four questions to settle it. They are the same four we go through when a customer sends us drawings.
1. What is the widest lamination in your core range?
Look at the widest piece across all the core designs you intend to build on the line, not only the current best-seller. In a three-limb core this is usually the centre limb or the yoke. The width class must cover that piece with a small margin, because strip width is the one thing a line cannot be adjusted beyond.
Then look at the narrowest piece. Each class also has a minimum strip width, set by how narrow a strip the feed rollers and edge guides can control. If your range spans very narrow and very wide pieces, it can be better to run two smaller lines than one large line that spends most of its time on narrow strip.
| Class | Strip width, approx. | Typical use |
|---|---|---|
| 200 | from about 45–50 mm up to 220 mm | Small distribution transformer cores; the most exported class in our range |
| 300 | from about 35–45 mm up to 320 mm | The mainstay class for distribution transformer cores |
| 400 | from about 40–50 mm up to 440 mm | Larger distribution and small power transformer cores |
| 600 | from about 70–80 mm up to 640 mm | Medium power transformer cores |
| 800 | from about 100 mm up to 820 mm | 110 kV-class power transformer cores |
| 1000 | from about 120 mm up to 1,020 mm | 220 kV-class cores, typically four-corner mitred designs |
Exact minimum and maximum widths vary with the configuration of each line, so treat the table as a first cut and confirm against the specification tab on the standard line or high-speed line page for the class you are considering.
2. Do your laminations have holes, and how many?
The number of hole punching stations follows from the core design. Modern distribution cores are usually clamped without bolt holes and need no hole punch at all. Larger cores and older designs may need two or more holes per lamination, which adds punching stations to the line. This does not change the width class, but it changes the line length and the price, so it belongs in the same conversation. Zero to four hole punches are available across the range.
3. How many tonnes a month, and on how many shifts?
Tonnage decides between the standard (step-feed) and the high-speed (continuous-feed) version within a class. The rule we apply: above roughly 300 tonnes a month, or between 100 and 300 tonnes a month on two shifts, the high-speed version is the right choice; below that, a standard line usually has the capacity to spare. Standard vs high-speed cut-to-length lines explains where the difference comes from.
Two things people sometimes get wrong here. First, peak strip speed is not output; what matters is laminations per shift, which depends on piece length, programme structure and how the line is fed. Second, tonnage per month is only half the story: the number of core types per month matters as much, because every programme change costs minutes on any line.
4. How much floor do you have, and where is the crane?
A line grows in length with each station added and in width with the class. As a reference point, a 1000-class line with a double-head decoiler occupies roughly 32 by 8 metres and weighs about 45 tonnes; a 200- or 300-class line fits in a fraction of that. Beyond the machine itself, allow space for coil storage at the decoiler end, for forklift access to the stacking tables, and for the finished stacks to be moved to core assembly. Crane capacity has to cover the heaviest coil you will load, which on the large classes is around five tonnes.
Options that do not change the class but do change the line
Once the class is fixed, the remaining choices are configuration. Left- or right-hand layout, to match the flow of your shop. Two to four decoiler heads, so the next strip is loaded while the current one runs. One or two V-notch stations, depending on yoke geometry and whether the core is stacked automatically. Stacking tables in 1+1, 3+3 or 5+5 arrangement, or an extended sorting chain on high-speed lines. Control system brand, paint colour, and the optional PLS terminal that generates cutting programmes from lamination drawings. These are listed on each product page and in the online line selector, which walks through the same questions and returns a first configuration.
What to send us for a firm proposal
Lamination drawings for your largest and your most common core, the strip thickness and grade you run, your monthly tonnage and shift pattern, and a sketch of the available floor area with the crane marked. From that we return a line proposal with knife and punch layout and a floor plan. If you would rather start with a rough configuration, the 行选择器 takes about five minutes.
Frequently asked questions
Can a line cut strip narrower than its minimum?
Not reliably. Below the minimum width the edge guides and feed rollers lose control of the strip and length accuracy suffers. If you regularly need very narrow strip, say so at the enquiry stage so the guiding can be specified for it.
Is it better to buy one 600 line or two 300 lines?
It depends on the width distribution of your cores. If most laminations are under 320 mm and only a few designs need more, two 300 lines give more total output and redundancy; if the wide designs are the volume, one 600 line is the better buy. Send the drawings and we will run both cases.
Which class is the most common?
In our range the 300 class is the mainstay for distribution transformer plants, the 400 class is the flagship for plants that also build small power transformers, and the 200 class is the one we export most.